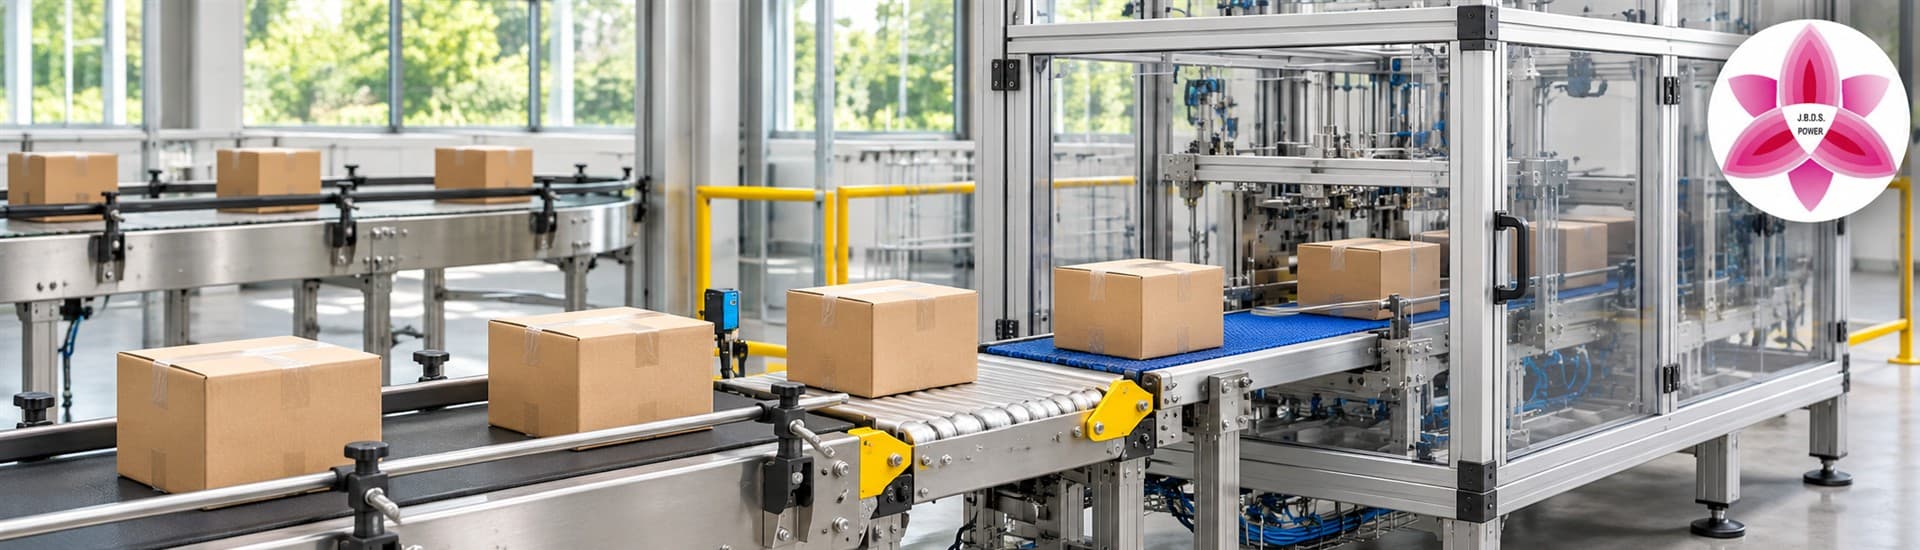
Conveyor Transfer Points: How to Plan a Smoother Handoff
The line runs well until a small carton reaches the next belt. It turns slightly, catches the guide and makes the carton behind it stop. An operator gets the line moving again, but the same problem returns with the next batch. If that sounds familiar, start by looking at the few centimetres where one piece of equipment hands the product to another.
A conveyor transfer point is the junction between two conveying surfaces or between a conveyor and a machine. The product, the equipment and the timing all meet there. Looking at those three together gives your team a better starting point than guessing which conveyor needs to change.
Watch what happens just before the handoff
Observe several runs from the normal, guarded operating position. Note the product variant, its orientation, whether the line was starting or already running, and what happened immediately before the stop. Ask the operator to describe the first thing they see. A carton that turns before it reaches the junction calls for a different investigation from one that catches at the junction.
Record how often the issue occurs and what a good transfer looks like. Even a short observation log can help a supplier reproduce an intermittent problem instead of testing only the easiest condition.

Bring the products that are hardest to transfer
A large, flat carton may cross a junction cleanly while a smaller carton dips at the same point. A pouch with a loose edge behaves differently from a rigid box, and a tall pack can react differently when it changes speed. Give the supplier samples that represent what actually runs, including light, short or less rigid packs.
Share the product dimensions, weight range and expected orientation. Include photos of the underside and any seams, feet or protrusions that could meet the transfer surface. If packaging changes across batches, explain which variation is normal and which is a defect.

Review the gap, height and alignment together
Ask the conveyor designer to inspect the end of the sending surface and the start of the receiving surface as a pair. A product needs suitable support while it crosses. The shape of the product base, the difference in height and the alignment of the two sections can all affect how it enters the next machine.
There are several ways to design a transfer, including close belt ends and powered transfer arrangements. The right approach depends on the products and the application. Give the supplier a side view of the junction and the available space, and ask how the proposed design will support your smallest or least stable product. See the conveyor specification checklist for other details to share.

Check what the receiving machine is ready to accept
Imagine a label applicator that pauses briefly while the upstream belt keeps bringing cartons. The first carton may cross perfectly and the fifth may arrive before there is room. That is a timing issue worth discussing even if the transfer geometry looks right.
Share how the receiving machine signals that it is ready, what the upstream line does during a pause and where products are allowed to queue. Ask the controls team to review arrival spacing, restart behaviour and the conditions that should stop the feed. A test at steady speed tells only part of the story. Include normal starts, stops and changes in production rate.

Make recovery part of the design review
Ask the people who operate and maintain the line how they recognise a transfer problem today. Can they tell where it started? Do they have enough information on the operator panel to call the right person? These are practical questions to settle alongside the equipment layout.
Agree who will review guarding, access and approved recovery procedures. Include those responsibilities in the handover, along with routine cleaning and inspection points. When a fault returns, a clear description of the symptom and operating condition is more useful than a general note that the conveyor jammed.

Agree what a successful transfer test looks like
Before ordering equipment or changing a line, agree on the sample range, operating conditions and observations to record. You might ask the supplier to demonstrate the smallest carton, the lightest pack and the format that tends to turn, then repeat the checks during a normal stop and restart. Record which formats and conditions were covered.
For an enquiry, bring a line sketch, product samples, the expected rate and a description of the failure. If the next machine sets the pace, include its infeed requirements. Explore JBDS Power conveyor customization or share your transfer point with the team.

Images are illustrative concepts. Transfer details depend on the products and the application.